0% READ
FULL TEXT
INTRODUCTION
Valsartan is a new potent, highly selective and orally active antihypertensive angiotensin II type 1 receptor antagonists (Saydam and takka, 2007). It acts by relaxing blood vessels and causing them to widen, which lowers blood pressure and improves blood flow (Katzung and Trevor, 2020). Valsartan is a BCS Class IV drug ( Lara et al., 2020). Valsartan is rapidly absorbed after oral administration (Thürmann, 2000). Tmax of valsartan ranges 2-4 hr (Wu, Q, et al., 2020). and then decline with a terminal half-life reported in various studies in the range of 6-9 hr.
With Conventional formulations, due to immediate release of drug, they have shorter duration of action which required multiple dosing (Loftsson, 2015). Specially concern for chronic diseases like hypertension, frequent dosing leads to poor patient compliance (Srivastava, K., et al., 2013). Noncompliance with current medication regimens is a significant challenge in India, especially with Immediate Release (IR) formulations (Ingersoll and Cohen, 2008).
In contrast to conventional immediate release dosage form, Controlled release formulation becoming more prevalent and effective not only due to extended release of drug and lack of frequent dosing but also improved safety of drug (Adepu and Ramakrishna, 2021). Controlled release formulation can be formulated as Single-Unit Dosage Forms (SUDF) or Multiple-Unit Dosage Forms (MUDF) (Nihad et al., 2018). Single unit dosage form contains active substance in tablet or as powder in capsules, on the other hand multiple-unit dosage forms contains more than one sub-units like pellets or mini-tablets etc. (Priese et al., 2023). Multiple unit dosage forms have advantage over single unit dosage form like more predictable gastric emptying, low intra or inter individual variability, lower risk of overdose and local irritation, gastric emptying less depend on nutritional status etc. (Ezgi et al., 2017). However, compared to Single-Unit Dosage Forms (SUDF), Multiple-Unit Dosage Forms (MUDF) are more complex technology requiring sophisticated manufacturing equipment like fluid bed processor, hot melt extruder, Extrusion and Spheronization etc. (Hannlie et al., 2017). As compared to tablets formulation, with current multiple-unit dosage technology which needs to be filled in capsules requires high production cost and low production rate. Another fact, with capsule filled multi-unit dosage the size of dosage form increases which again an issue for dosage administration and patient compliance over tablet formulation (Mistry and Batchelor, 2017). With multiunit dosage form a pellet, compression in to tablet again is a challenge due to damage to polymer layer due to non-flexibility or addition of cushioning agent to increase cost and size of tablet. On the other hand, multiunit pellet technology is having known issue of segregation due to density differences leading to content uniformity problems etc.
To overcome the challenge of flexible film coat, different methods have been reported like increase the plasticity of coat (Thao and Phuong, 2019) and varying amount of polymer on the pellet (Dwibhashyam and Ratna, 2008).
In the current study design, immediate release granules of valsartan were used as the immediate release component, while the Ethyl cellulose (matrix) coating (Prakash et al., 2018) was used for the slow (controlled) release component of the multi-unit dosage forms, which were manufactured using wet granulation and fluid bed processors, respectively. The effect of drying temperature utilizing a fluidized bed processor was investigated for the release rate of valsartan. The release of valsartan obtained by RDCR was analyzed using nonlinear regression analysis, release rate constant, and other kinetic parameters, and compared to immediate release component of valsartan (Figure 1).
MATERIALS AND METHODS
Materials
Valsartan (VAL) was obtained as a gift sample from Harman Finochem Ltd., Chatrapati Sambhaji Nagar, India. Commercially available Hypromellose (METHOCEL™ E5 Premium LV) and Hypromellose (Methocel K4M premium DC) as a gift sample from Colorcon, Mumbai, India, was used as a binding agent and release controlling agent respectively. Release controlling polymer, Ethyl cellulose 20 cps (Ecolose N20) and 7 cps (Ecolose N7) were obtained from Nucell Pharma Corp, USA. Triethyl Citrate used as plasticizer obtained as gift sample from Mamata polycoats, India. Micronized Talc used as flow aid obtained from IMERYS, France Crospovidone (Polyplasdone™ XL-10) used as super-disintegrant obtained as gift sample from Ashland suppliers, India. Microcrystalline cellulose (Ceolus KG 802) used as cushioning agent obtained from Asahi Kasei, India. Colloidal Silicon Dioxide (Aerosil 200) used as glident obtained from Evonik India. Magnesium stearate is used as lubricant obtained from Peter grevens, USA. Double distilled water was used throughout the experiment. Analytical grade chemicals and reagents were used for analysis.
Methods
Wet granulation technique - granules preparation
During the development of the RDCR tablets, granules components were manufactured using conventional wet granulation technique. Optimization of Hypromellose (METHOCEL™ E5 Premium LV) was performed using 1.2% w/w, 2.4% w/w and 3.3% w/w concentration for batch number F53, F54, and F55 respectively.
A 200 g valsartan was co-sifted with lactose monohydrate, mixed with Rapid Mixer Granulator (RMG) (Make:Bectochem). The binder solution of Hypromellose (Methoocel E5) was prepared using purified water as solvent. The dry mix then granulated with binder solution of Hypromellose (Methoocel E5). The resultant granules were dried using Fluid Bed Dryer (FBD) (Make: Dr. Pharm) at 50ºC for 1 hr to moisture content of 3.5±0.5% w/w. The composition of formulation trials was explained in Table 1.
| Batch Number | F53 | F54 | F55 | F56 | F57 | F58 | F59 | F60 | F61 | |||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Sl. No. | Ingredient | mg/tab | mg/tab | |||||||||||||
| (I) | IR Granules Optimization | RDCR Granules Optimization | ||||||||||||||
| 1. | Valsartan | 40.0 | 40.0 | 40.0 | 40.0 | 40.0 | 40.0 | 40.0 | 40.0 | 40.0 | ||||||
| 2. | Lactose Monohydrate | 81.5 | 80.0 | 79.0 | 79.0 | 79.0 | 79.0 | 79.0 | 79.0 | 79.0 | ||||||
| 3. | HPMC E-5 cps | 1.5 | 3.0 | 4.0 | 4.0 | 4.0 | 4.0 | 4.0 | 4.0 | 4.0 | ||||||
| 4. | P. Water | q.s | q.s | q.s | q.s | q.s | q.s | q.s | q.s | q.s | ||||||
| IR granules (Subtotal) | 123.0 | 123.0 | 123.0 | 123.0 | 123.0 | 123.0 | 123.0 | 123.0 | 123.0 | |||||||
| (II) | RDCR Granules | |||||||||||||||
| 5. | Ethyl cellulose 20 cps | NA | NA | NA | -- | -- | -- | 4.79 | 7.79 | 15.0 | ||||||
| 6. | Ethyl cellulose 7 cps | NA | NA | NA | 10.0 | 20.0 | 30.0 | -- | -- | -- | ||||||
| 7. | Triethyl Citrate (TEC) | NA | NA | NA | 1.5 | 3.0 | 4.5 | 0.70 | 1.14 | 1.5 | ||||||
| 8. | Micronized Talc | NA | NA | NA | 3.0 | 3.0 | 3.0 | 3.00 | 3.0 | 3.0 | ||||||
| 9. | Isopropyl alcohol | NA | NA | NA | q.s | q.s | q.s | q.s | q.s | q.s | ||||||
| ER Granules (Subtotal) | NA | NA | NA | 137.5 | 149.0 | 160.5 | 131.5 | 134.9 | 142.5 | |||||||
| (III) | Extra-granular Part | |||||||||||||||
| 10. | Crospovidone XL 10 | NA | NA | NA | 12.0 | 12.0 | 12.0 | 12.0 | 12.0 | 12.0 | ||||||
| 11. | Talc | NA | NA | NA | 2.0 | 2.0 | 2.0 | 2.0 | 2.0 | 2.0 | ||||||
| 12. | Ceolus KG 802 | NA | NA | NA | 35.5 | 24.0 | 12.5 | 41.5 | 38.1 | 30.5 | ||||||
| 13. | Magnesium stearate | NA | NA | NA | 1.0 | 1.0 | 1.0 | 1.0 | 1.0 | 1.0 | ||||||
| Total | NA | NA | NA | 188.0 | 188.0 | 188.0 | 188.0 | 188.0 | 188.0 | |||||||
| Physicochemical tests | Granules | Compressed tablet | ||||||||||||||
| Tensile strengths (N) | NA | NA | NA | 45-55 | 45-55 | 45-55 | 45-55 | 45-55 | 45-55 | |||||||
| Friability | 0.54 | 0.45 | 0.12 | 0.495 | 0.52 | 0.53 | 0.51 | 0.53 | 0.41 | |||||||
| Disintegration time (Sec) | NA | NA | NA | 21 | 27 | 32 | 31 | 29 | 30 | |||||||
| Powder Flow Properties | ||||||||||||||||
| Sieve No/ Mean Dp,j | PSD % Distribution | Ethyl cellulose 7 CPS | Ethyl cellulose 20 CPS | |||||||||||||
| Batch Number→ | F53 | F54 | F55 | F56 | F57 | F58 | F59 | F60G | F60T | F61 | ||||||
| Pan (84 µm) | 6 | 1 | 25 | 62 | 30 | 26 | 31 | 25 | 29 | 17 | ||||||
| 100 (141 µm) | 23 | 2 | 25 | 84 | 56 | 40 | 54 | 43 | 47 | 28 | ||||||
| 60(214 µm) | 17 | 3 | 14 | 96 | 70 | 52 | 69 | 57 | 60 | 34 | ||||||
| 40(335 µm) | 16 | 4 | 14 | 99 | 80 | 68 | 79 | 67 | 72 | 42 | ||||||
| 30(564 µm) | 15 | 6 | 13 | 105 | 90 | 80 | 90 | 78 | 82 | 51 | ||||||
| 20(854 µm) | 23 | 8 | 9 | 108 | 95 | 85 | 100 | 84 | 88 | 56 | ||||||
| Bulk Density | 0.511 | 10 | 0.521 | -- | 101 | 93 | 102 | 90 | 94 | 63 | ||||||
| Tap Density | 0.619 | 12 | 0.641 | -- | -- | 100 | 103 | 94 | 97 | 70 | ||||||
| Compressibility Index | 17.45 | 18 | 18.72 | -- | -- | -- | 105 | 96 | 100 | 75 | ||||||
| Hausner ratio | 1.21 | 1.20 | 1.23 | G: Granules, T: Tablets | ||||||||||||
The resultant granules were evaluated for flow properties, friability and Particle Size Distribution (PSD).
Determination of Particle Size Distributions of IR granules
Particle size analyses were performed on samples of the dried granules using a nest of sieves and an electromagnetic sieving machine (Make: Electrolab) equipped with sieve No.: 20, 30, #40, #60, #100.
Determination of Granules Friability
Granule friability testing is used to measure the strength of granules. 10 g sample of granules is weighed and sifted through ASTM sieve # 100, the retained quantity of granules was weighed, and transferred to USP friability tester. USP friability tester is rotated 100 times using a speed from 24 to 26 rpm. The granules from drum sifted through ASTM sieve # 100 and retained granules were accurately weighed. The friability of granules was calculated as per equation below:
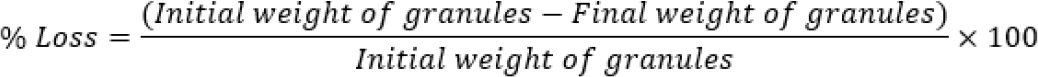
Preparation of RDCR granules
To control release of VAL, the IR granules were coated with release controlling polymer ethyl cellulose 7cps and 20 cps.
The Coating solution was prepared by adding ethyl cellulose to a vessel containing Isopropyl alcohol, along with Triethyl citrate as plasticizer, and micronized talc. The hydration time maintained was 2 hr. The composition of formulation is detailed in Table 1.
Preparation of CR granules with Ethyl cellulose 7 CPS
A 615 g of IR granules from batch No. F55 was added to Fluid bed processor (Make: Solid Lab 1) and coated with Binder solution containing Ethyl cellulose (7 CPS) with concentration to unlubricated ER granules ranges from 7.3%w/w. 13.4%w/w and 18.5%w/w for batch no. F56, F57 and F58 respectively.
Preparation of CR granules with Ethyl cellulose 20 CPS
A 615 g of IR granules from batch No. F55 was added to Fluid bed processor (Make: Solid Lab 1) and coated with Binder solution containing Ethyl cellulose (20 CPS) with concentration to unlubricated ER granules ranges from 3.7%w/w. 5.9%w/w and 10.6% w/w for batch no. F59, F60 and F61 respectively.
Drying of granulate coated with ethyl cellulose with Triethyl Citrate (TEC)
The granulate then dried at 35ºC for 1 hr in a Fluidized bed dryer (Make: Solid Lab 1) to moisture content of 3.5±0.5% w/w. and curing was performed at 45ºC ± 3ºC.
Lubrication of Controlled Release Granules
The resultant dried granules were mixed with Crospovidone XL 10, micronized talc, microcrystalline cellulose (Ceolus KG 802) for 10 min using octagonal blender (Make: Sainath) and lubricated with magnesium stearate with 2 min.
Tableting
Lubricated granules of batch No. F60 were subjected to tableting using 8.0 mm circular shape punches fitted with single rotatory compression machine (Make: Parle). The physical parameter of compressed tablets was presented in Table 1.
Evaluation of Tablet Tensile Strength (T)
The Hardness of ten tablets were determined individually using Erweka Hardness tester and compiled in Table 1.
Evaluation of Disintegration Time (DT)
The disintegration time of the RDCR tablets was determined following the procedure outlined in USP Chapter <701>. One dosage unit was placed in each of the six tubes of the disintegration basket without using a disk. The disintegration apparatus was operated with water as the immersion fluid, maintained at 37 ± 2ºC.
The time required for each tablet to completely disintegrate into small particles, leaving no palpable residue, was recorded. Measurements were performed on six tablets (n=6). The observed disintegration time was 20 sec ± 0.2 sec, as illustrated in Figure 2.
Dissolution test
The method described by Sridevi Ramachandran (Sridevi, Badal Kumar, & Sameer G, 2014) was followed for the dissolution study. One tablet was placed in 1000 mL of dissolution medium consisting of pH 6.8 phosphate buffer, maintained at a temperature of 37 ± 2ºC. The medium was stirred using a USP Apparatus II (paddle) at a speed of 50 rpm.
At predetermined time intervals, 13 mL aliquots of the dissolution medium were withdrawn using an auto titrator. The samples were filtered, appropriately diluted with blank dissolution medium, and analyzed for Valsartan content. The analysis was performed using a UV-visible spectrophotometer (Shimadzu Corporation) at a wavelength (λmax) of 230 nm.
Statistical Analysis
To understand and evaluate the mechanism of drug release of VAL through Ethyl cellulose and its different grades, dissolution profile obtained from different formulation were mathematically evaluated with first order, zero order, Hixson-Crowell, Korsmeyer-Peppas and Higuchi dissolution model (Yong, et al., 2010). The choice of an appropriate model for fitting dissolution data is critical, not only for quantitative evaluation of drug release characteristics but also for comparing dissolution profiles using model-dependent tools. A number of statistical criteria for evaluating the goodness of fit of a model, including the correlation coefficient (R_obs-pre), the coefficient of determination (Rsqr, R2, or COD), the adjusted coefficient of determination (Rsqr_adj or R2 adjusted), the Mean Square Error (MSE), the standard deviation of the residuals (MSE_root or Sy.x), SS, WSS, the Akaike Information Criterion (AIC), and the Model Selection Criterion (MSC). Among these criteria, the most popular ones in the field of dissolution model identification are the R2 adjusted, the AIC, and the MSC.
For release models with the same number of parameters, the coefficient of determination (R2) can be used to discriminate the most appropriate model. However, when comparing models with different numbers of parameters, the adjusted coefficient of determination should be used:
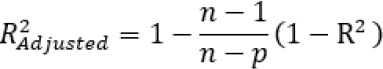
where n is the number of data points and p is the number of parameters in the model.
The Akaike Information Criterion (AIC) is an estimator of prediction errors and thereby is relative quality of statistical models for a given set of data. Given a collection of models for the data, AIC estimates the quality of each model, relative to each of the other models. Thus, AIC provides a means for model selection.
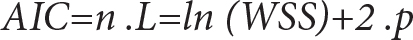
where n is the number of data points, WSS is the weighted sum of squares, and p is the number of parameters in the model.
MSC is a statistical model selection criterion used for dissolution data modeling, which is calculated using equations below.
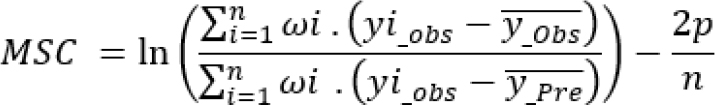
where wi is the weighting factor, which is usually equal to 1 for fitting dissolution data, yi_obs is the ith observed y value, yi_pre is the ith predicted y value, equation M50 is the mean of all observed y-data points, p is the number of parameters in the model, and n is the number of data points. The MSC is a modified reciprocal form of the AIC and has been normalized so that it is independent of the scaling of the data points.
RESULTS
Evaluation of granules Particle size distribution of IR Granules
The results of Particle size distribution for selection of IR granules are tabulated below in Table 1.
Evaluation of granules flow properties and friability
The results of granules flow properties and friability for selection of IR granules are tabulated in Table 1. The granules friability of batch no. F55 is lower than batch no. F53 and F54.
Drying of granulate coated with ethyl cellulose with Triethyl Citrate (TEC)
A coating solution comprising ethyl cellulose as the release-controlling polymer and Triethyl Citrate (TEC) in an organic solvent (isopropyl alcohol) was used to coat the IR granules. Achieving an optimal drying temperature is essential to ensure that solvent evaporation occurs gradually. This controlled evaporation allows the polymer particles to coalesce effectively, minimizing the risk of agglomeration and drug migration. As a result, a uniform coating with a smooth surface is formed on the granules. Such surface uniformity is crucial for achieving the desired sustained release effect of the polymer. The sustained release of Valsartan (VAL) is demonstrated effectively at the proposed optimum bed temperature of 35 ± 2ºC.
Drug release profiles of Controlled release formulation
Granules coated with ethyl cellulose with 7cps grades (Batch no. F56, F57 and F58) were evaluated release of VAL. The dissolution results show Table 1 more than 85% drug release in 6 hr.
In contrast, granules coated with ethyl cellulose with 20cps grades (Batch no. F59, F60 and F61) were evaluated for release of VAL. The dissolution results of Batch no. F59 shows faster release, releasing 100% VAL in 8 hr., conversely F61 shows incomplete release profile with 75% release at the end of 18 hr’ dissolution studies, however batch no. F59 shows complete release i.e. 96% at the end of 18 hr’ dissolution studies.
Tablet Disintegration Times, Tensile Strength And Friability
The Disintegration Times (DT), Tensile strengths (T) and friability for the formulation F56, F57, F58, F59, F60 and F61 are presented in Table 1. In order to exclude the effect on hardness, all the formulation was compressed with hardness ranging from 45N to 55N with friability ranging from 0.4% to 0.5%.
When tested for disintegration study, the tablets were found to disintegrate within a minute Figure 3 to de-aggregation of granules floating in disintegration vessel, which confirms that the formulation batch No. F56, F57, F58, F60, F61 and F59 are fast disintegrating multi-particulate dosage form.
RDCR Tablet dissolution study and comparison with RDCR granules
The Dissolution behavior of Batch No. F60 (RDCR Tablets) was studied using i-Disso dissolution technology. Initial quick disintegration of tablets into granules was observed. The initial disintegration and extended dissolution of granules is clear by dispersion in the dissolution vessel as well as dissolution data. Table 1 above represents dissolution data comparing F60 RDCR Granules and F60 RDCR Tablets showing no significant difference in granules integrity after compression process.
RDCR Tablet dissolution study using i-Disso
Tablet disintegration with distributed granules is clearly visible starting at 1 hr. From 2 hr to 10 hr demonstrate gradual release of VAL by diffusion for up to 10 hr with up to 90% release of VAL. At end of 18 hr about 96% of the VAL was released at the end of the dissolution testing. The release of VAL and the full expansion of the polymer cause a change in the density and porosity of the granules, resulting in their dispersion in the dissolution vessel.
Comparative drug release profile of RDCR formulation vs Conventional Matrix formulation on drug release of VAL
To compare the drug release profile of RDCR technology with conventional matrix release technology, a formulation was developed with conventional matrix formulation containing VAL. A batch is manufactured using IR granules as per Batch No. 55,
The IR granules was further blended in bin blender with Hypromellose (Methocel K4M DC), Microcrystalline cellulose (Avicel PH 102) and Colloidal silicon dioxide (Aerosil 200) for 20 min and lubricated with pre-sifted Magnesium stearate for 3 min. The lubricated blend is then subjected to tableting using 7.8 mm circular shape punches fitted with single rotatory compression machine (Make: Parle). The physical parameter of compressed tablets was presented in Table 2.
| Batch No. → | F60T | F62 | |||
|---|---|---|---|---|---|
| Manufacturing Formula | |||||
| Sl. No. | Ingredient | Mg/tab | %w/w | Mg/tab | %w/w |
| Intra granular Material | |||||
| 1. | Valsartan | 40 | 21 | 40 | 20 |
| 2. | Lactose Monohydrate | 79 | 42 | 79 | 40 |
| 3. | HPMC E-5 cps | 4 | 2 | 4 | 2 |
| Subtotal | 123 | 65 | 123 | 62 | |
| Extra-granular Material | |||||
| 4. | Hypromellose (Methocel K4M premium DC) | 0 | 0 | 70 | 35 |
| 5. | Ethyl cellulose 20 cps | 7.79 | 4 | -- | -- |
| 6. | Triethyl Citrate (TEC) | 1.14 | 1 | -- | -- |
| 7. | Micronized Talc | 3 | 2 | -- | -- |
| 8. | Isopropyl alcohol | q.s | |||
| 9. | ER Granules (Subtotal) | 134.93 | 72 | 193 | 97 |
| 10. | Crospovidone XL 10 | 12 | 6 | -- | -- |
| 11. | Talc | 2 | 1 | -- | -- |
| 12. | Ceolus KG 802 | 38.1 | 20 | -- | -- |
| 13. | Colloidal Silicon Dioxide (Aerosil 200) | -- | -- | 5 | 3 |
| 14. | Magnesium stearate | 1 | 1 | 2 | 1 |
| Total | 188.03 | 100 | 200 | 100 | |
| Physicochemical tests | |||||
| 1. | Avg Weight (mg) | 182.4 to 191 | 200 to 209 | ||
| 2. | Tensile strengths (N) | 45-55 | 55 | ||
| 3. | Friability (%) | 0.41 | 0.01 | ||
| Comparative Drug Release study | |||||
| Time (Hours) | % Dissolution | ||||
| 1 | 29 | 30 | |||
| 2 | 47 | 35 | |||
| 3 | 60 | 42 | |||
| 4 | 72 | 49 | |||
| 6 | 82 | 60 | |||
| 8 | 88 | 73 | |||
| 10 | 94 | 86 | |||
| 12 | 97 | 96 | |||
| 18 | 100 | 101 | |||
DISCUSSION
Evaluation of granules Particle size distribution of IR Granules
Batch F55 exhibits the highest proportion of coarse granules, with 23% of particles measuring at 854 µm, complemented by a balanced distribution of mid-sized granules ranging from 141 to 564 µm, while only 6% are classified as fines (less than 100 µm). This distribution suggests that Batch F55 likely represents the endpoint of high-shear granulation, where stable growth granules are essential for ensuring optimal granules coating performance in FBP. In contrast, Batch F54 is characterized by the highest no of fines, comprising 26% of particles under 100 µm, alongside a substantial presence of mid-sized granules and moderately coarse granules at 19% for those measuring 854 µm or greater. This composition indicates possible undergrowth or insufficient granulation time and energy, which may adversely affect granules coating performance in FBP. Batch F53 presents a similar profile to F54 with fines, but it contains a significantly reduced proportion of coarse particles at only 9%. The majority of granules in this batch fall within the mid-size range of 214 to 564 µm, suggesting a balanced but skewed distribution towards smaller particles, which could facilitate faster dissolution while simultaneously posing a risk of increased dust and fines content
Evaluation of granule flow properties and friability
The analysis of friability across all batches indicates low values, reflecting good mechanical stability. Notably, Batch F55 exhibits the lowest friability at 0.12%, signifying it as the hardest and most robust option. In terms of densities and flow characteristics, both bulk and tap densities remain consistent among the batches, with F54 and F55 displaying slightly greater density than F53. The Compressibility Index (CI) values range from approximately 17% to 19%, categorizing the flow properties from “fair” to “good,” although F55, with a CI of around 18.7%, indicates slightly reduced flowability. The Hausner Ratio (HR) falls between 1.20 and 1.23, consistent with fair flow characteristics, where F55 again demonstrates the least favorable flow properties with the highest HR of 1.23. In comparing the batches, F55 is distinguished by its robustness, evidenced by its low friability, yet it concurrently possesses the acceptable flow properties as indicated by its elevated CI and HR. Conversely, Batch F54 presents a more balanced profile, showcasing commendable toughness alongside marginally improved flow attributes, characterized by the lowest HR and CI. Batch F53, however, is noted to exhibit the weakest structural integrity and flow capacity among the three. In conclusion, considering mechanical strength, Batch F55 is the optimal choice hence selected for further process
Drug release profiles of Controlled release formulation
The analysis of drug release profile of formulation F56, F57, F58, F59, F60, and F61 provides a comprehensive overview of the dissolution characteristics of various formulations. The formulations F56, F57, and F58 are composed of Ethyl Cellulose 7 cps, which results in lower viscosity and facilitate faster hydration and disintegration. In contrast, F59, F60, and F61 utilize Ethyl Cellulose 20 cps, characterized by higher viscosity leading to a slower drug release profile. The concentration of TEC, a plasticizer, increases with the polymer concentration to maintain film flexibility.
Notably, within the group of formulations with a CPS of 7, an increase in coating percentage is associated with a slower release profile, as evidenced by the rapid release of F56, compared to the more gradual release observed in F57 and F58. Specifically, after 1 hr, F56 achieved a release of 62%, while F57 and F58 exhibited 30% and 26%, respectively. This trend continues over 8 hr, with F56 reaching 108% release compared to F57’s 95% and F58’s 85%. In contrast, when comparing formulations of differing viscosity 20 CPS but similar coating levels, such as F58 (7 CPS) and F61 (20 CPS), F61 demonstrated a slower drug release rate despite the lower coating level. After 1 hr, F58 released 26% compared to F61's 17%, and after 8 hr, F58 released 85% while F61 released only 56%. This indicates that higher viscosity, reflective of a more viscous polymer, results in denser and less permeable films, thereby impeding drug release even at reduced coating levels.
The influence of TEC as a plasticizer enhances film flexibility, though the predominant factor affecting release is the viscosity and concentration of the polymer. The interpretation of the results indicates that F56-F58 are ideal for rapid disintegration, achieving over 90% release within 6 hr, while F59-F61 are more suitable for controlled release applications, particularly F60, which demonstrates significant sustained release along with complete release at 18 hr. time point, making it an optimal choice for extended drug release
Cross-comparison of formulations further confirms these trends, highlighting that while both viscosity and % w/w coating significantly influence drug release rates, viscosity appears to exert a more pronounced effect, particularly evident in the comparison of F61 (10.5% w/w at 20 CPS) being slower than F58 (18.6% w/w at 7 CPS). Thus, it can be concluded that while both factors are critical, the viscosity of the polymer may play a more crucial role in regulating the rate of drug release
In the process of narrowing down to suitable candidates, it is evident that only F58 and F60 fulfil the target criteria of achieving an effectiveness range of 80-90% at the 8-hr mark. F58 demonstrates an 85% effectiveness at 8 hr and a full 100% at 12 hr, characterized by a high coating level and a more permeable film due to its lower viscosity of 7 cps and weight/weight ratio of 18.6%. This formulation offers a smoother release curve extending through the 12-hr period. Conversely, F60, which has a viscosity of 20 CPS and a weight/weight ratio of 5.8%, achieves an effectiveness of 84% at 8 hr and 94% at 12 hr. Its moderate coating level results in a denser film, making it a cost-effective option that is more robust for scaling up
The F60 formulation, with a concentration of 20 CPS and a 5.8% composition, has been optimized to achieve a target release of 80-90% within an 8-hr timeframe. This formulation not only ensures controlled release but also provides a regulatory safety margin extending to 12 hr. Additionally, it features a lower coating load, which contributes to cost efficiency, and offers improved scalability for various applications.
Tablet Disintegration Times, Tensile Strength And Friability
The tabulated data reveals that the tensile strength across all batches consistently falls within the acceptable range of 45-55 N, indicating uniform tablet hardness. Regarding friability, all measured values are below 1.0%, adhering to pharmacopeial limits. Notably, batch F61 exhibits the lowest friability at 0.414%, suggesting superior mechanical resistance, while batch F60, with a friability of 0.529%, remains acceptable despite being the highest in this analysis. The disintegration time ranges all batches disintegrating well under 1 min, which is optimal for rapid disintegration formulations; F56 stands out as the fastest disintegrating batch. In conclusion, all batches meet the fundamental mechanical and disintegration criteria, with F61 being the best overall due to its lowest friability and acceptable disintegration time of 30 sec, while F56 excels in rapid disintegration at 21 sec, albeit with slightly higher friability.
Evaluation of drug release from hydrophilic matrix tablets
To anticipate the drug release mechanism and kinetics, the in vitro release data was applied together with several kinetic models. The drug release mechanism from different formulations were studied using DDSOLVER software application (Jieyu, Yuan, Nadia, & Raimar, 2014).
The mathematical equations were used for model selection for dissolution. The dissolution modelling results are found as explained in Table 3. The analysis of key metrics reveals important insights into model performance across different batches. The adjusted R² (R²_adj) serves as an indicator of goodness-of-fit, where higher values are preferable. The Root Mean Square Error (RMSE) reflects the typical prediction error, with lower values indicating better accuracy. The Akaike Information Criterion (AIC) balances model fit and complexity, where a lower score is more favorable. Additionally, the Model Selection Criterion (MSC) suggests that higher values are indicative of superior model selection
| Batch No. | B. No. F59 | B. No. F60 | B. No. F61 | |||||||||
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Dissolution Modelling | Rsqr | MSE | AIC | MSC | Rsqr | MSE | AIC | MSC | Rsqr | MSE | AIC | MSC |
| Zero Order | -1.04 | 1358.16 | 85.64 | -0.94 | -0.4482 | 876.5895 | 81.6993 | -0.5926 | 0.2770 | 280.3480 | 71.4393 | 0.1022 |
| 1st Order | 0.9853 | 9.7560 | 41.2159 | 3.9993 | 0.9888 | 6.7809 | 37.9419 | 4.2694 | 0.8870 | 43.8131 | 54.7344 | 1.9583 |
| Higuchi | 0.6801 | 212.670 | 68.953 | 0.917 | 0.8256 | 105.5740 | 62.6497 | 1.5241 | 0.9698 | 11.7231 | 42.8690 | 3.2766 |
| Korsmeyer-Peppas | 0.8819 | 89.705 | 61.982 | 1.692 | 0.9173 | 57.1874 | 57.9302 | 2.0484 | 0.9763 | 10.5026 | 42.6778 | 3.2979 |
| Hixson-Crowell | 0.9107 | 59.340 | 57.465 | 2.194 | 0.9358 | 38.8644 | 53.6557 | 2.5234 | 0.7837 | 83.8651 | 60.5779 | 1.3090 |
| Hoffenberg | 0.9896 | 7.8761 | 40.0876 | 4.1247 | 0.9888 | 7.7547 | 39.9479 | 4.0465 | 0.8868 | 50.1509 | 56.7485 | 1.7345 |
| Baker-Lonsdale Model | 0.8199 | 119.6974 | 63.7797 | 1.4923 | 0.9622 | 22.8583 | 48.8788 | 3.0541 | 0.9796 | 7.8993 | 39.3160 | 3.6714 |
| Makoid-Banakar | 0.9901 | 8.7524 | 41.6498 | 3.9511 | 0.9935 | 5.2484 | 37.0471 | 4.3688 | 0.9963 | 1.9276 | 28.0325 | 4.9251 |
| Peppas-Sahlin Model | 0.9861 | 12.3450 | 44.7451 | 3.6072 | 0.9913 | 7.0227 | 39.6682 | 4.0776 | 0.9964 | 1.8674 | 27.7468 | 4.9569 |
| Quadratic | 0.6998 | 228.1119 | 70.3817 | 0.7587 | 0.8156 | 127.5379 | 65.1489 | 1.2464 | 0.9134 | 38.3881 | 54.3429 | 2.0018 |
| Weibull Model | 0.9888 | 9.9467 | 42.8010 | 3.8232 | 0.9985 | 1.1983 | 23.7539 | 5.8458 | 0.9952 | 2.4932 | 30.3481 | 4.6679 |
| Logistic | 0.9636 | 27.6559 | 51.3917 | 2.8687 | 0.9951 | 3.3589 | 32.4178 | 4.8832 | 0.9947 | 2.3418 | 29.1714 | 4.7986 |
| Gompertz | 0.9413 | 44.6007 | 55.6929 | 2.3908 | 0.9801 | 13.7741 | 45.1183 | 3.4720 | 0.9829 | 7.5788 | 39.7414 | 3.6242 |
| Probit | 0.9741 | 19.6403 | 48.3115 | 3.2110 | 0.9971 | 1.9885 | 27.6995 | 5.4074 | 0.9941 | 2.6366 | 30.2385 | 4.6800 |
The data is a summary analysis and model comparison for the dissolution data modeling of batches F59, F60, and F61, evaluated against key statistical indicators: R² (goodness-of-fit), MSE (mean square error), AIC (Akaike Information Criterion), and MSC (Model Selection Criterion).
For formulation F59, the Hoffenberg model emerged as the best fit, exhibiting the highest R² of 0.9896, the lowest AIC of 40.09, and the highest MSC of 4.12, while other strong contenders included Makoid-Banakar, Weibull, and Peppas-Sahlin. Conversely, the Zero-order and Higuchi models demonstrated poor fits, reflected by low R² values and high Mean Squared Error (MSE).
In formulation F60, the Weibull model was identified as the optimal fit, achieving an R² of 0.9985, an AIC of 23.75, and an MSC of 5.85, with close alternatives being Probit, Gompertz, and Logistic models, all showing strong fits. Again, the Zero-order model fell short, yielding a negative R².
For formulation F61, the Peppas-Sahlin model was the best fit, with an R² of 0.9964, an AIC of 27.75, and an MSC of 4.96, while Makoid-Banakar, Weibull, and Logistic models also provided excellent fits. Notably, Zero-order and first-order models exhibited relatively weak fits, marked by higher MSE and lower R² values.
General observations indicate that the zero-order model exhibited poor fit across all batches, while the first-order, Hoffenberg, Weibull, and Makoid-Banakar models consistently demonstrated strong performances. Notably, the Weibull model showed universal strength, particularly for Batch F60, while the Peppas-Sahlin and Makoid-Banakar models effectively captured complex release kinetics. Models like Hixson-Crowell, Korsmeyer-Peppas, and Baker-Lonsdale performed moderately but did not achieve the top rankings. In conclusion, for publication or modeling purposes, it is recommended to utilize the Makoid-Banakar or Peppas-Sahlin models for Batches F59 and F61, and the Weibull model for Batch F60, as these provide the best statistical strength and are suitable for controlled or extended-release formulations. The analysis of drug release from the formulations of Valsartan indicates that advanced, non-linear kinetic models provide superior fits compared to classical linear models.
Moderate fits were seen in Zero, Logistic, Probit, and Hixson-Crowell models, whereas Hoffenberg and Quadratic models were the least suitable. Mechanistically, Zero Order demonstrates a constant release, often yielding poor fits, while First Order reflects release proportional to the remaining drug. Higuchi exhibits diffusion-driven release, and Hixson-Crowell focuses on changing surface area. The Korsmeyer-Peppas model uses an exponent to characterize the release mechanism, indicating Fickian diffusion for n values less than 0.45 and anomalous behavior for values between 0.45 and 0.89.
Hybrid models like Hoffenberg, Peppas-Sahlin, and Makoid-Banakar incorporate diffusion and erosion. Statistical models such as Weibull, Logistic, Gompertz, and Probit provide flexibility but lack mechanistic depth. The mechanistic parameters from the analysis show that batch F59 has an n value of 0.322 indicating a sigmoidal/mixed release, while F60 and F61 exhibit Fickian diffusion and near-anomalous behaviors, respectively. The parameter β in F59 suggests an S-shaped release, while values less than one in F60 and F61 align with diffusion, and slight positive lag times in F60 and F61 indicate early-stage delays.
In conclusion, consistent surfaces and diffusion characteristics suggest that hybrid and statistical models best describe the release mechanisms, with F59 showing multi-phase release patterns, while F60 and F61 trend toward simpler diffusion is influenced by formulation changes. Future monitoring of n, β, and Ti was performed to track shifts in release mechanisms, and visualizing trends enhanced clarity in the analysis.
The analysis of drug release from the formulations of Valsartan indicates that advanced, non-linear kinetic models provide superior fits compared to classical linear models. Overall, the consistent performance of non-linear models such as Hoffenberg, Weibull, Peppas-Sahlin, and Makoid-Banakar across the formulations underscores their effectiveness in capturing the complex drug release kinetics influenced by matrix characteristics and the interplay of diffusion and erosion mechanisms. The reliance on adjusted R², AIC, and MSC was critical in determining the optimal model, particularly when comparing models with varying numbers of parameters. In conclusion, the drug release kinetics of Valsartan from the tested formulations are best characterized by sophisticated non-linear models, reinforcing the complexity of the underlying mechanisms.
The evaluation of model performance reveals that a lower Mean Squared Error (MSE), represented by greener shades, signifies a better fit for the data.
Among the various models assessed, the Peppas-Sahlin Model, Makoid-Banakar Model, Weibull Model, Probit Model, and Logistic Model stand out as the best performers, exhibiting the lowest MSE across all batches. In contrast, models such as Zero Order and Quadratic demonstrate significantly high MSE values, which indicates a poor fit to the data.
RDCR Tablet dissolution study and comparison with RDCR granules
Upon analyzing the drug release profile, it was observed that the release data indicates a slightly faster drug release for the tablets compared to the granules, particularly in the early phase from 0 to 4 hr. For instance, at the 2-hr time point, the granules achieved a release of 43%, while the tablets reached 47%. In the middle phase, from 4 to 10 hr, the tablets consistently outperformed the granules by approximately 4 to 5%, demonstrating a controlled yet quicker release rate. By the late phase, both formulations approach complete drug release, with the tablets achieving 100% release by 18 hr. This analysis suggests that the F60 Tablets provide a marginally faster release profile throughout the testing period, which may indicate effect of compression during tableting process as well as flexibility of granules coat and effect of cushioning agent to protect granules during compression process. Overall, both systems achieve near-complete drug release by the end of the observation period. The overall statistics indicate that the mean for f2 is 69.06. This value of f2 falls within the range of [50,100], situated between the mean of R and the mean of T. Consequently, the similarity between R and T can be accepted based on these findings.
Comparative drug release profile of RDCR formulation vs Conventional Matrix formulation on drug release of VAL
From Figure 2, it is observed that the Conventional VAL Matrix ER formulation follows Zero order kinetics however VAL RDCR granules follow the First order kinetics. Both technologies show controlled release without initial burst release. The lower RSD values of VAL RDCR confer low variability between tablet to tablet than Conventional VAL Matrix ER formulation.
The updated drug release profile comparing F60 and F62 over time in hours indicates notable differences in their release characteristics. F60, which employs a multi-unit particulate system, demonstrates a more gradual and sustained release of the drug. In contrast, F62, utilizing a conventional matrix formulation, exhibits a more rapid release, particularly in the initial hours, and achieves a higher cumulative release at the 18-hr mark.
In the context of drug dissolution studies, a comparative analysis of Matrix HPMC-based Sustained Release (SR) systems versus RDCR sustained release systems reveals distinct differences. The drug release mechanism for HPMC-based systems involves swelling, diffusion, and erosion, where HPMC forms a gel layer that regulates drug release and exhibits less pH dependency due to its hydrophilic nature. In contrast, RDCR sustained release systems rely on diffusion through a semi-permeable polymer coat, demonstrating moderate pH sensitivity influenced by the contents of EC and pore-formers. Initial drug release may present a burst effect in HPMC systems if the drug is surface loaded, while RDCR sustained release systems can allow for controlled lag times depending on coating thickness. A dissolution profile comparison indicates that HPMC Matrix sustained release system initially releases approximately 30% of the drug at 1 hr, compared to 25% for RDCR sustained release systems, with HPMC showing faster release rates at earlier time points yet converging with RDCR sustained release systems at 12 to 18 hr. The advantages of HPMC systems include simple manufacturing and cost-effectiveness, albeit with susceptibility to dose dumping and risks of tablet breakage. Conversely, RDCR sustained release systems offer not only simple manufacturing and cost-effectiveness but also reduced inter-patient variability and tailored release profiles. Modeling insights suggest that while HPMC systems primarily exhibit diffusion-controlled release, RDCR sustained release systems may fit models indicating non-Fickian behavior, highlighting their unique release kinetics. Ultimately, HPMC Matrix SR is recommended for cost-efficiency and ease of manufacturing with moderate release control, while RDCR sustained release systems are advisable for applications prioritizing cost-efficiency and ease of manufacturing, consistent release, reduced variability, and enhanced patient safety
Stability studies
The RDCR tablets were packed in Alu Alu blister and stored at accelerated stability condition 40ºC ± 2ºC /75%± 5%RH for a period of 3 months, the RDCR tablets were analyzed for drug content, Organic Impurity, Water content and Dissolution studies. The results show the product is stable and complying with acceptance criteria.
CONCLUSION
The study has shown that wet granulation and fluid bed coating is an effective approach for retarding drug release from the resultant matrix particles. Tableting rather than encapsulation of the matrix particles is more effective in prolonging the release. The release profile can be best optimized by coating with ethyl cellulose 20 cps with concentration of 7.79 mg/tab along with TEC 1.14 mg/tab which gave a controlled release dose (40 mg) for time (18 hr). The RDCR offers advantages over other current technologies such as MUPS, Palletization, Extrusion Spheronization, and is more robust in terms of content uniformity, control over drug release and uniformity, tableting qualities, and production costs. The RDCR granules can be utilized for manufacturing different dosage forms like tablets, sachets, powder for oral suspension etc.